

 Türkçe
 Русский
 Español
 العربية
Hydraulic Cylinders for Injection Molding Machines
An injection molding machine runs thousands of cycles a day, and every one of them depends on hydraulic cylinders: to close and lock the mould, inject the melt, eject the part and pull cores. Fast, repeatable motion with low friction and no leakage is what matters here.
Fenitsa supplies tie-rod and custom cylinders for moulding machines and moulds — including replacements for machines whose original cylinders are no longer available.
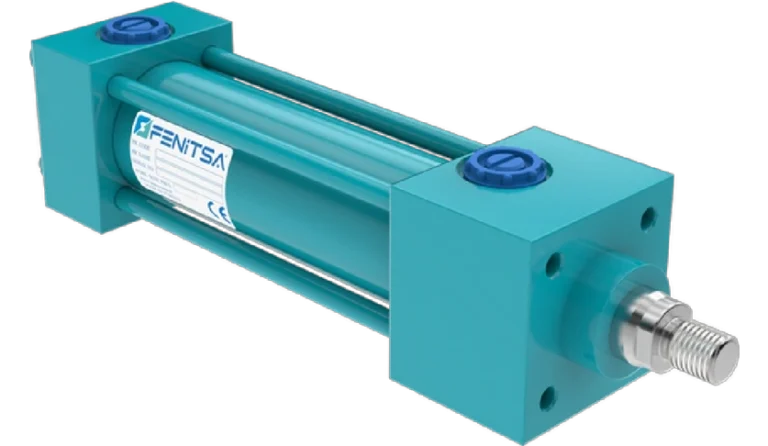
Cylinders on an Injection Molding Machine
| Cylinder | What it does | Key requirement |
|---|---|---|
| Clamp / locking | Closes and holds the mould against injection pressure | High force, rigid mounting |
| Injection | Drives the screw forward to fill the cavity | Precise speed and pressure control |
| Carriage (nozzle) | Moves the injection unit to the mould | Moderate force, frequent cycles |
| Ejector | Pushes the part off the mould | Short, fast strokes |
| Core pull | Moves side cores inside the mould | Compact size, heat near the mould |
Worked Example: Clamp Force and Bore
A part with 400 cm² projected area moulded at an average cavity pressure of 400 bar needs a clamp force of 400 × 400 × 0.1 ≈ 1,600 kN (≈ 163 t). A direct hydraulic clamp at 160 bar would need a theoretical bore of 357 mm — the next standard size is ØNone mm.
Many machines use a toggle mechanism so a smaller cylinder can generate the locking force; in that case the cylinder is sized for the toggle geometry, not the full clamp force.
What to Specify for Moulding Cylinders
- Temperature near the mouldCore-pull cylinders sit close to hot tooling; the high-temperature seal package (up to +200 °C) may be needed.
- Low frictionSmooth motion at low speed for injection and ejection.
- Cycle countSeal and bearing choice for millions of cycles.
- Compact mountingsFlange or body mountings that fit inside the mould base.
Our standard hydraulic series are built for 160 bar working and 240 bar test pressure with a 250 bar option, bores from Ø40 to Ø200 mm and strokes up to 5,000 mm, using honed St52 tube and Ck45 rods hard-chrome plated to at least 20 µm. Anything outside that envelope is engineered as a custom cylinder.
Which Fenitsa Cylinder Fits Which Function?
Inspection Routine
What to check, and how often, in this application.
- Every mould changeCheck core-pull cylinders for leaks and hose damage near hot tooling.
- MonthlyCheck clamp cylinder for oil at the rod and consistent clamp pressure.
- Every 6 monthsTest ejector and core-pull cylinders for drift and sticking.
- YearlyReseal high-cycle cylinders before leaks affect part quality.
Hydraulic Cylinders for Injection Molding Machines – FAQ
Can you replace the clamp cylinder of an old injection molding machine?
Yes. Send the dimensions or the old cylinder; we reverse-engineer it and build a replacement to an approved drawing.
Which cylinders do moulds use for core pulling?
Compact block or flange-mounted hydraulic cylinders; near hot tooling, specify the temperature so seals can be selected.
How is clamp force calculated?
Projected part area × cavity pressure. 400 cm² at 400 bar needs about 1,600 kN (≈ 163 t).
Do you supply locking cylinders?
Yes — locking and clamp cylinders are built to drawing; send bore, stroke, pressure and mounting details.
Send Your Application Data
Bore, rod, stroke, pressure, mountings and quantity — or a drawing or photo of the existing cylinder. We reply with a technical proposal and quotation from our plant.