
 Türkçe
 Русский
 Español
 العربية
FDH SERIESSTANDARD
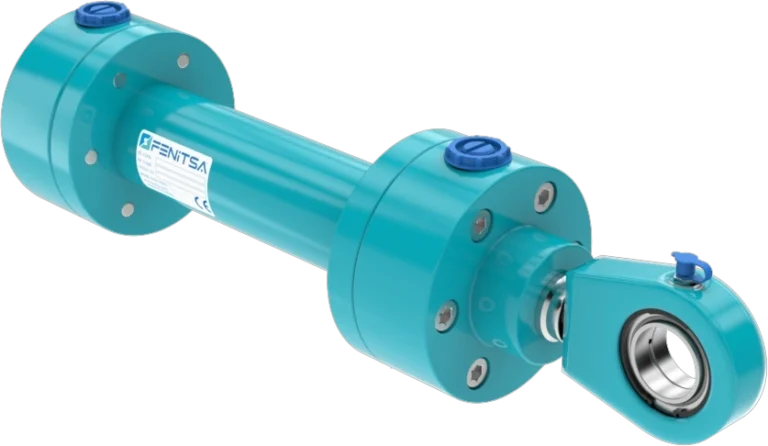
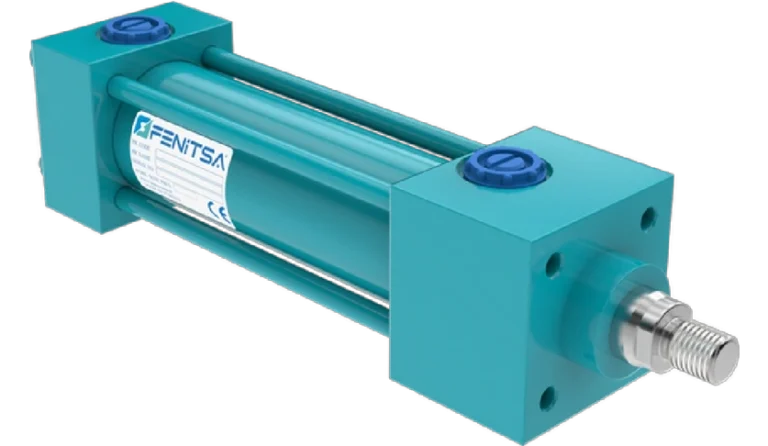
FDH Type Hydraulic Cylinder
General-purpose industrial cylinder with foot, clevis, flange and trunnion mounting options.
Ø40 – Ø200 mm
Bore
Ø28 – Ø125 mm
Rod
up to 5,000 mm
Stroke

Fenitsa designs and manufactures hydraulic cylinders for machine builders, OEMs and maintenance teams. Our range covers tie-rod, welded and heavy-duty cylinders from Ø40 to Ø200 mm bore with strokes up to 5,000 mm, plus telescopic and fully custom designs built to your drawing.
Based in Konya, Türkiye, we have been making hydraulic cylinders since 1979. Every unit is assembled and pressure tested in-house before it leaves the plant.
General-purpose industrial cylinder with foot, clevis, flange and trunnion mounting options.
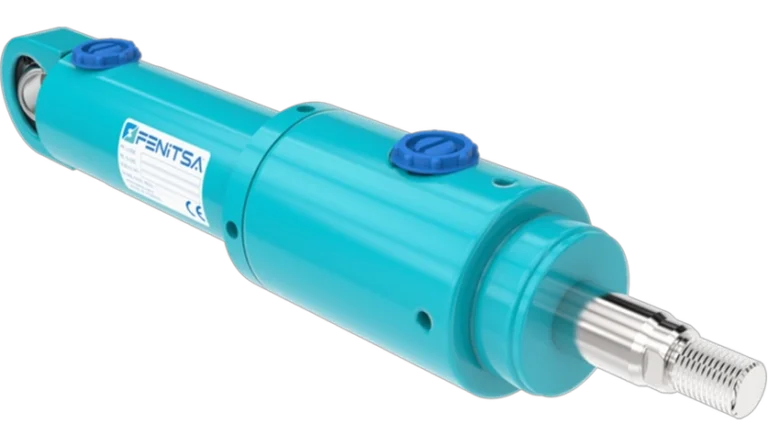
Heavy-duty design for mobile equipment and harsh operating conditions.
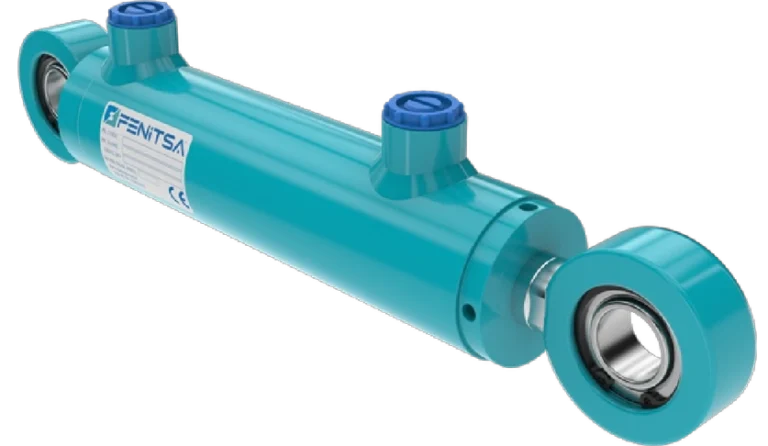
Welded body for compact machines and space-critical installations.
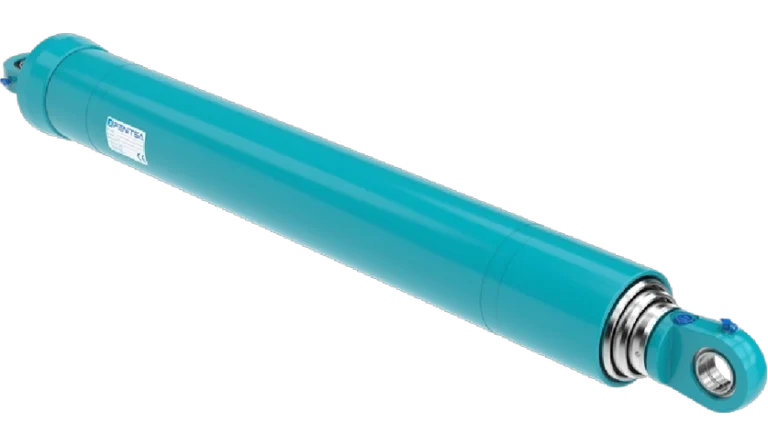
Long stroke from a short retracted length; stages and bores sized per project.
Double rod, tandem and adjustable-stroke versions for synchronised or precise motion.
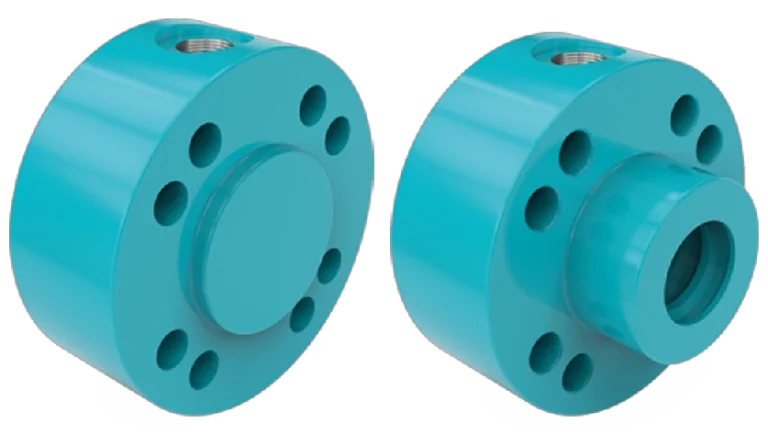
Heads and end caps for service, repair and custom cylinder builds.
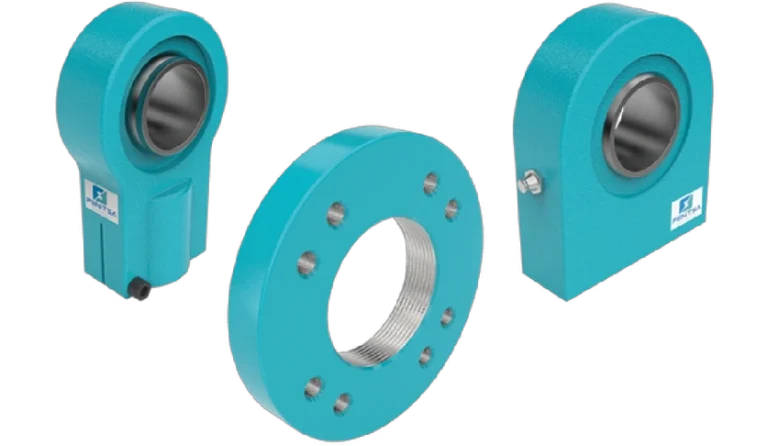
Clevises, rod eyes, flanges, feet and trunnions matched to the cylinder.
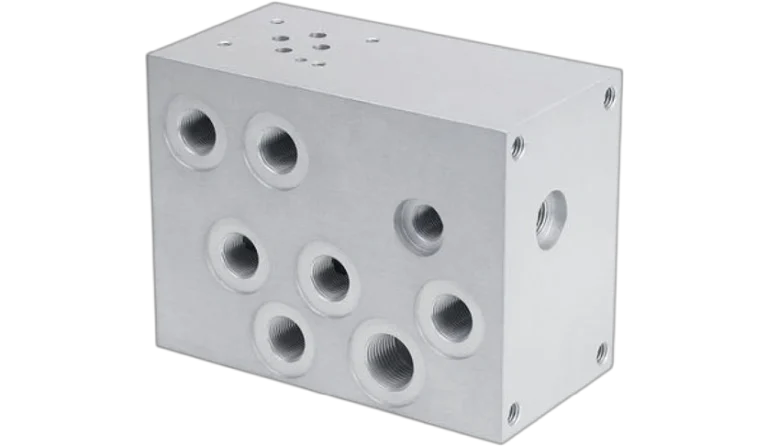
Manifold blocks for compact, serviceable hydraulic circuits.
Common specification of the FDH, KHS, THS and tie-rod series.
| Parameter | Standard series |
|---|---|
| Cylinder tube | Honed St52 (E355) seamless steel tube |
| Piston rod | Ck45 (C45) steel, hard chrome plated ≥ 20 µm, f7 tolerance |
| Working / test pressure | 160 bar (2,320 psi) / 240 bar (3,480 psi); 250 bar (3,625 psi) option |
| Bore / rod range | Ø40, 50, 63, 80, 100, 125, 160, 200 mm / Ø28 – Ø125 mm |
| Stroke | Standard 100 – 500 mm, up to 5,000 mm |
| Speed | up to 0.5 m/s (standard seals) |
| Temperature | −20 °C to +80 °C; −30 °C to +200 °C with special seals |
| Mountings | Foot, rear clevis, front/rear flange, front/rear trunnion, rod eye |
These values describe the catalogue series. Higher pressures, larger bores, longer strokes, stainless rods or other seal compounds are quoted as custom builds. For force at a given pressure, use our free hydraulic cylinder force calculator.
Choosing the construction that suits your machine.
| Type | How it is built | Best for |
|---|---|---|
| Tie-rod | Heads clamped to the tube by external steel tie-rods; easy to dismantle and reseal | Industrial machines, presses, automation; easy field service |
| Welded body | End cap welded to the tube, head threaded or bolted; no tie-rods | Mobile and agricultural machines where space and weight are limited |
| Heavy-duty (mill type) | Bolted flanged heads, thick-walled tube | Shock loads, steel mills, mining and continuous heavy service |
| Telescopic | Two or more nested stages extending in sequence | Tippers, lifts and platforms needing long stroke from a short body |
| Double rod / tandem | Rod through both heads, or two pistons in line | Equal speed both ways, synchronised motion or more force from a small bore |
The welded vs tie-rod comparison explains the trade-offs in more detail.
Quick reference for sizing the bore.
| Bore | kN | metric tons | lbf |
|---|---|---|---|
| Ø40 mm (1.57 in) | 20.1 | 2.1 | 4,520 |
| Ø50 mm (1.97 in) | 31.4 | 3.2 | 7,063 |
| Ø63 mm (2.48 in) | 49.9 | 5.1 | 11,213 |
| Ø80 mm (3.15 in) | 80.4 | 8.2 | 18,080 |
| Ø100 mm (3.94 in) | 125.7 | 12.8 | 28,250 |
| Ø125 mm (4.92 in) | 196.3 | 20.0 | 44,141 |
| Ø160 mm (6.30 in) | 321.7 | 32.8 | 72,321 |
| Ø200 mm (7.87 in) | 502.7 | 51.3 | 113,001 |
Values are theoretical (F = P × A). Allow 20–30 % margin for friction and dynamic loads, and remember that pull force is lower because the rod area is subtracted.
Casting, moulding, CNC machining, painting, assembly and testing take place in one plant, so dimensions and lead times do not depend on a chain of subcontractors.
Hydraulic cylinder production since 1979 and serial production since 1985 — the experience behind every drawing we release.
CAD/CAM design since 1996. Our engineers check bore, rod buckling and mounting loads before a drawing is released for production.
Quality management system certified since 2008. Each cylinder is pressure tested; test and material records can be supplied with the shipment.
Catalogue series for fast supply and custom cylinders for the positions where a standard part will not fit — on the same quotation.
You talk to the people who build your cylinder: quotations, drawings and delivery dates come straight from the plant.
From raw tube to tested cylinder.
Your requirements are converted into a production drawing: bore, rod, stroke, mountings, ports, cushioning and seal package.
Honed St52 tube and hard-chrome-plated Ck45 rod (≥ 20 µm, f7) are cut and machined to the drawing length.
Heads, pistons, caps and mounting parts are machined on CNC turning and machining centres, with robotic cells on repeat parts.
Seals are fitted in a clean area; tie-rods are torqued or the body is welded according to the series.
Each cylinder is cycled and held at test pressure (240 bar for the 160 bar series) to check internal and external leakage.
Primer and top coat, ports plugged, and the cylinder is packed for road, sea or air freight.
Photos of each step are on our production page.
Cylinders sized for the load, duty cycle and environment of each application.
Press cylinders with large bores and rigid flange mounting for forming, baling and compacting.
Clamping and ejector cylinders with low-friction seals for fast, repeatable cycles.
Heavy-duty cylinders with thick-walled tubes and rod protection for abrasive dust.
Marine cylinders with paint systems and seals selected for humid, salty environments.
Long-stroke gate cylinders designed for slow, controlled movement and long idle periods.
Agricultural and excavator cylinders for mobile machines exposed to shock loads.
Typical path from enquiry to series supply.
Bore, rod, stroke, pressure, mountings and quantity — or a drawing or photo of the cylinder you use today.
We confirm the design, point out risks such as rod buckling, and quote price and lead time.
You approve the production drawing. For new designs we recommend a first-article or sample order.
Cylinders are built, pressure tested and documented.
Packed for export and shipped on the Incoterm agreed with your purchasing team; repeat orders follow the approved drawing.
Not sure which cylinder you need? Our guide to how hydraulic cylinders work and the double-acting / single-acting comparisons are a good starting point.
See our neutral guide to the top hydraulic cylinder manufacturers worldwide and in Türkiye, and the checklist for sourcing from Turkey.
A manufacturer. Parts are cast, moulded and machined on our CNC and robotic lines, and every cylinder is assembled, painted and pressure tested at our plant in Konya Organised Industrial Zone, Türkiye. We have been making hydraulic cylinders since 1979.
Tie-rod, welded body and heavy-duty mill-type cylinders (FDH, KHS, THS series), telescopic cylinders and special tie-rod designs with double rod, tandem or adjustable stroke, plus covers, mounting parts and hydraulic blocks. See the hydraulic cylinder range.
Yes. We supply machine builders who order the same cylinder repeatedly. Series orders are produced to an approved drawing, so every batch has the same dimensions, seal package and test record.
Yes — special bores, strokes, mountings, port positions and seal materials are routine for us. The process is described on our custom hydraulic cylinders page.
Bore, rod diameter, stroke, working pressure, mounting style at both ends, quantity and the application. A drawing or photo of an existing cylinder speeds things up considerably.
Yes. Fenitsa ships to customers in Europe and the Middle East, including Germany, France, Spain, Iraq and Saudi Arabia. Our guide to sourcing from Turkey covers logistics and documentation.
Share bore, rod, stroke, pressure, mountings and quantity. Drawings (PDF, DWG, STEP) and photos are welcome.